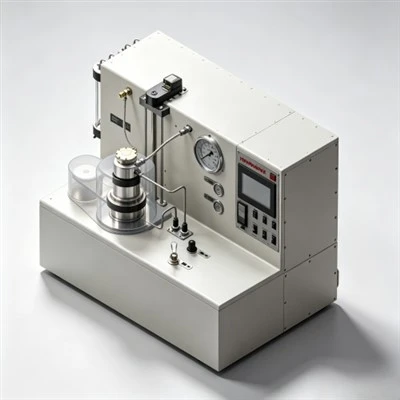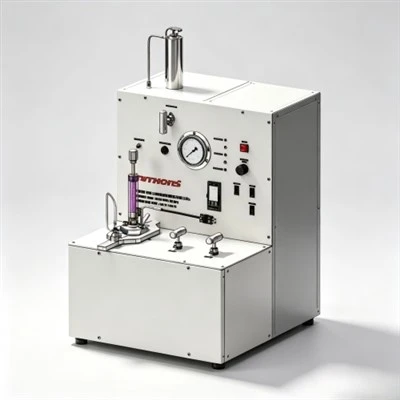

When petroleum procurement directors and cementing specialists evaluate what is the price of a cementing retarder, they assess a cost spectrum ranging from standard lignosulfonates ($1.50 to $3.50 per kilogram) to advanced synthetic AMPS terpolymers ($8.00 to $18.00+ per kilogram) tailored for severe deepwater and ultra-HPHT reservoirs across the Middle East, the Gulf of Mexico, and the Tarim Basin. Exploring what is the price of a cementing retarder reveals that unit chemical procurement accounts for only a minor fraction of overall well construction risk; an inadequate, low-cost retarder that undergoes thermal degradation downhole can trigger premature flash setting inside casing strings, inducing lost circulation and catastrophic multimillion-dollar sidetracking operations. By analyzing what is the price of a cementing retarder through the lens of active chemical purity, thermal operating limits, dosage efficiency, and API Spec 10A laboratory compliance, operating companies balance initial chemical expenditure against total job safety, ensuring reliable pumpability and life-of-well annular zonal isolation.

The Operational Imperative of Retarder Economics in Modern Well Construction
In petroleum exploration and completion engineering, primary cementing represents the permanent mechanical barrier that anchors the casing string within the borehole, isolates porous hydrocarbon formations, protects shallow drinking water aquifers from cross-contamination, and shields casing steel from corrosive downhole brines containing hydrogen sulfide (H₂S) and carbon dioxide (CO₂). However, displacing cement slurry across deep wellbores requires circulating the fluid through thousands of meters of narrow tubulars and upward into the annular space. As the slurry descends, it transitions from ambient surface temperatures to bottom-hole circulating temperatures (BHCT) that can exceed 160°C to 200°C (320°F to 392°F), under confining hydrostatic pressures surpassing 80 to 120 MPa (11,600 to 17,400 psi).
Under these intense thermal and barometric loads, uninhibited Portland cement clinker minerals-primarily tricalcium silicate (C₃S) and tricalcium aluminate (C₃A)-hydrate rapidly. The accelerated dissolution of calcium and aluminate ions into the aqueous phase causes immediate nucleation of interlocking calcium silicate hydrate (C-S-H) gel fibers. If slurry pumpability is compromised downhole, apparent viscosity surges, elevating equivalent circulating density (ECD) beyond formation fracture limits. The resulting lost circulation leaves productive intervals un-cemented. In extreme scenarios, flash setting inside casing strings traps drill pipe, inducing non-productive time (NPT) costs that exceed millions of dollars.
Consequently, exploring what is the price of a cementing retarder requires moving past simplistic per-ton invoice figures to evaluate life-of-well operational economics. Chemical retarders provide the technical insurance policy that guarantees an engineered placement safety window-typically 90 to 120 minutes beyond calculated displacement times. Understanding how chemical synthesis, raw material grade, and thermal thresholds govern market pricing enables drilling engineers and procurement managers to select the most cost-effective additive package that mitigates downhole risks while preventing unnecessary waiting-on-cement (WOC) downtime on high-spread-rate offshore and onshore drilling rigs.
1. Core Factors Determining the Market Price of Cementing Retarders
The commercial valuation of oilfield cementing retarders is driven by underlying chemical synthesis complexity, active polymer concentration, and performance testing compliance:
- Chemical Backbone and Molecular Architecture: Naturally derived by-products like unmodified calcium or sodium lignosulfonates require minimal refining and command the lowest entry-level prices. Conversely, synthetic terpolymers synthesized from high-purity 2-acrylamido-2-methylpropane sulfonic acid (AMPS), acrylic acid, and maleic anhydride require multi-step precision polymerization under controlled temperatures and catalysts, driving manufacturing costs higher.
- Thermal Operating Thresholds: Additives rated for conventional applications below 120°C (248°F) utilize standard organic backbones that hydrolyze under severe heat. Retarders engineered for ultra-HPHT environments (180°C to 230°C+) incorporate thermally stable sulfonate and phosphonate functional groups that resist degradation, requiring premium raw materials and rigorous thermal stability qualification.
- Active Solids Concentration and Product Form: Liquid retarders provide ease of mixing on offshore rigs but incur higher freight costs per active kilogram due to water weight. High-purity spray-dried powders offer maximum active concentration (typically >92% active content), lowering international shipping expenses but requiring specialized precision blending equipment at onshore bulk plants.
- Dosage Efficiency and Sensitivity Profiles: A high-performance synthetic retarder functioning effectively at 0.3% to 0.8% by weight of cement (BWOC) often proves more commercially economical per barrel of slurry than an unrefined lignosulfonate requiring 1.5% to 3.0% BWOC to achieve equivalent pumpability.
- Quality Control and API Monogram Compliance: Premium manufacturers conduct exhaustive batch-specific quality assurance adhering to API Spec 10A and API RP 10B-2. Verifying thickening time repeatability on calibrated HPHT consistometers across multiple cement clinker batches adds analytical labor and equipment overhead that is reflected in commercial pricing.
2. Commercial Pricing Matrix Across Primary Retarder Chemical Families
To assist procurement specialists and cementing engineers in estimating chemical budgets, the table below outlines global commercial benchmarks, active chemistries, operational temperature ranges, and typical application envelopes:
3. Unit Chemical Cost vs. Total Job Cost: The Dosage Efficiency Equation
A frequent pitfall in procurement management is focusing exclusively on the invoice price per kilogram rather than the effective cost per cubic meter of slurry pumped. Low-cost lignosulfonates possess relatively low molecular activity. Under demanding downhole temperatures, achieving a 5-hour thickening window requires heavy additive concentrations (often 1.8% to 2.5% BWOC). In contrast, high-tier synthetic AMPS polymers provide powerful surface adsorption at concentrations of only 0.4% to 0.7% BWOC.
The mathematical reality becomes evident when evaluating chemical consumption across a typical 50-ton (1,000-sack) production liner cementing operation:
As the comparative data demonstrates, deploying high-efficiency synthetic polymers reduces total chemical mass by over 75%, resulting in direct procurement savings while significantly reducing rig-site chemical storage footprint and logistics costs.
Regional Application Case: Deep Carbonate Sour Gas Production Liner Cementing in the Ahwaz Field, Khuzestan Province, Iran
Case Application: Ahwaz Oilfield, Khuzestan Province, Southwestern Iran

Target Formation: Deep HPHT Khami Sour Gas Carbonates (High Pressure, High H₂S & Narrow ECD Window)
Regional Cementing Background in Khuzestan Carbonate Plays
In the Ahwaz field of southwestern Iran, drilling operations penetrate overpressured gas-bearing carbonate reservoirs within the Cretaceous-Jurassic Khami Group. Well measured depths regularly exceed 4,900 to 5,300 meters (16,000 to 17,400 feet). Downhole conditions are severe: bottom-hole static temperatures (BHST) climb to 165°C to 175°C (329°F to 347°F) with formation pressures exceeding 12,000 psi (82.7 MPa). The formations produce sour gas containing H₂S (up to 6%) and CO₂ (up to 8%). Cementing 7-inch production liners across the Khami interval requires heavy Class G slurry systems (1.98 to 2.10 g/cm³) weighted with barite and stabilized by high-temperature polymers.
Regional Cementing Challenges in Extreme HPHT Formations
Operators cementing deep production liners across the Khami formation encounter critical technical hurdles:
- Severe Retarder Sensitivity: At temperatures above 160°C, minor variations of 0.05% BWOC in chemical retarder concentration cause large swings in thickening time, risking premature flash setting or multi-day setting delays.
- Narrow Equivalent Circulating Density (ECD) Windows: Close margins between formation pore pressure and fracture breakdown pressure demand low-viscosity slurries that maintain steady rheology without premature gelation spikes.
- Risk of Sour Gas Channeling: An extended transition time during slurry phase changes allows sour gas invasion into the decaying hydrostatic column, creating sustained casing pressure (SCP).
Technical Requirements for Slurry Qualification
To qualify a heavy 1.98 g/cm³ (16.5 ppg) Class G cement system across the Khami gas zone, the operator established strict performance criteria:
- Thickening time validation on an HPHT consistometer confirming a pumpability window of 5 hours and 30 minutes to 70 Bc under simulated dynamic ramp schedules.
- API fluid loss control strictly below 35 mL/30 min at 165°C using an automated high-temperature stirred fluid loss cell to prevent dehydration.
- Static gel strength (SGS) transition window (from 100 to 500 lbf/100 ft²) of less than 30 minutes, with 24-hour compressive strength exceeding 3,500 psi (24.1 MPa).
How Strategic Chemical Procurement Resolved the Commercial and Technical Challenge
In planning Well Ahwaz-412, the operator's procurement team initially analyzed what is the price of a cementing retarder based on unit price alone, opting for an inexpensive modified lignosulfonate priced at $3.20/kg. However, during pre-job HPHT consistometer qualification, the lignosulfonate suffered thermal degradation at 165°C. Even when the dosage was increased to 2.8% BWOC (which inflated chemical costs), the slurry exhibited severe premature gelation, thickening to 70 Bc in only 115 minutes and leaving zero safety margin for placement.
Recognizing that operational failure would incur drilling rig NPT exceeding $45,000 per day, the operator upgraded the chemical design to KELIOIL synthetic AMPS-based high-temperature retarders (priced at $11.80/kg). Laboratory testing confirmed that a low dosage of only 0.85% BWOC delivered an ideal right-angle set profile, maintaining a baseline consistency of 18 Bc for 4 hours and 30 minutes before rising sharply to 70 Bc at 5 hours and 38 minutes. Furthermore, ultrasonic testing on a UCA verified that the slurry developed 500 psi compressive strength in 9 hours and reached 3,850 psi at 24 hours.
During field execution, the slurry placed cleanly across the 1,050-meter liner without surface pressure surges or ECD spikes. Post-job radial acoustic cement bond logs (CBL-VDL) confirmed 100% circumferential bonding across the Khami sour gas pay zone. Subsequent negative pressure testing recorded zero sustained annular casing pressure, proving that evaluating what is the price of a cementing retarder from a total job risk perspective delivers far greater economic value than low-bid commodity purchases.

Pre-Purchase Laboratory Audits and Procurement Quality Protocols
To protect capital investments and guarantee downhole reliability, operating companies should mandate strict pre-purchase laboratory validation protocols:
- Chemical Active Purity and Ash Content Auditing: Require suppliers to provide Certificates of Analysis (COA) specifying active polymer solids content, moisture percentage, and residual inorganic ash content. Low-cost commodity retarders often contain up to 25% inert fillers that dilute chemical efficacy.
- API RP 10B-2 Thickening Time Verification: Conduct pre-shipment consistometer tests using delivered cement clinker and actual rig mix water. Thickening time curves must demonstrate linear performance and reproducible safety cushions within ±15 minutes across different manufacturing batches.
- Compressive Strength Analysis on UCA: Verify non-destructively that the retarder does not cause severe compressive strength retardation at bottom-hole static temperature (BHST). The slurry must attain 500 psi (3.45 MPa) compressive strength within 12 to 16 hours to prevent inflated waiting-on-cement rig costs.
- Packaging Integrity and Shelf-Life Guarantees: Ensure powder additives are packaged in multi-wall moisture-barrier paper bags with internal polyethylene liners (or UV-resistant bulk totes) to prevent clumping and hydrolytic degradation during maritime transit and tropical quayside storage.
Frequently Asked Questions (FAQ) Regarding Cementing Retarder Pricing
1. Why are synthetic polymer retarders significantly more expensive than lignosulfonates?
Synthetic polymer retarders utilize specialized monomer precursors-primarily AMPS, maleic anhydride, and acrylic acid-that undergo controlled solution or emulsion polymerization. This precision synthesis provides a thermally stable carbon-carbon backbone that withstands temperatures up to 230°C (446°F) without hydrolyzing, unlike unrefined lignosulfonates derived as inexpensive paper industry by-products.
2. How does freight and international packaging influence the landed price of retarders?
Liquid retarders contain 50% to 65% water, which significantly increases shipping costs per active chemical kilogram during international container transport. Highly concentrated dry powder retarders (>90% active content) reduce maritime container freight costs by up to 60%, offering superior landed value for remote onshore and offshore operations.
3. Can a cheap retarder cause waiting-on-cement (WOC) cost overruns?
Yes. Low-grade retarders often exhibit non-linear dosage responses. If slightly overdosed to survive high temperatures, they can permanently poison clinker hydration, preventing the cement from setting for 48 to 72 hours. On offshore drillships with spread rates exceeding $400,000 per day, a 24-hour WOC delay wipes out any initial savings achieved through cheap chemical procurement.
Strategic Recommendations for Chemical Procurement and Operations
As well drilling programs navigate deeper horizons, narrower hydraulic margins, and extreme geothermal gradients, establishing what is the price of a cementing retarder requires looking beyond basic product invoices to evaluate total job risk and performance value. Advanced synthetic retarders deliver predictable thickening kinetics, low active consumption, and rapid compressive strength development, providing unmatched technical and economic reliability.
KELIOIL remains dedicated to manufacturing high-performance oilfield cementing retarders under strict ISO 9001 and API Spec 10A quality control standards. By combining state-of-the-art polymer synthesis with comprehensive laboratory testing support, KELIOIL provides operators and cementing service contractors worldwide with dependable chemical solutions that guarantee wellbore integrity, environmental safety, and maximum asset productivity.
Optimize Your Cementing Additive Costs with KELIOIL Retarders
Our technical chemical specialists provide comprehensive slurry cost optimization audits, HPHT laboratory testing verification, and reliable bulk chemical supply of premium cementing retarders tailored to demanding onshore and offshore drilling operations.