
When petroleum exploration directors and drilling superintendents evaluate an Australia cementing service, they examine technical capabilities across complex offshore deepwater basins and onshore coal seam gas (CSG) plays, including the North West Shelf, Browse Basin, Cooper Basin, and the Surat Basin in Queensland. Selecting a qualified Australia cementing service requires navigating demanding downhole environments characterized by depths exceeding 5,000 meters, bottom-hole static temperatures (BHST) reaching 165°C, narrow equivalent circulating density (ECD) margins across fragile marine carbonates, and severe lost circulation risks in shallow underpressured coal cleats. By deploying an advanced Australia cementing service adhering to API Spec 10A and API RP 10B-2 testing standards, operators utilize specialized Class G cement slurries, synthetic polymer additives, and precision HPHT consistometer testing to prevent premature slurry setting, eliminate annular gas migration, eliminate sustained casing pressure (SCP), and guarantee multidecade well integrity.

The Operational Significance of Wellbore Cementing Across Australian Energy Basins
Australia's hydrocarbon landscape represents a dynamic mix of world-class offshore liquefied natural gas (LNG) export projects and extensive onshore unconventional gas development. Offshore drilling operations in Western Australia and the Northern Territory-centered in the Carnarvon, Browse, and Bonaparte basins-penetrate deep, overpressured, high-temperature gas-bearing horizons characterized by weak, highly permeable calcarenite and fractured carbonate layers. In contrast, eastern onshore operations in Queensland and New South Wales focus on coal seam gas (CSG) reservoirs, where thousands of production wells penetrate shallow, friable coal seams requiring low-density, non-damaging slurries that safeguard fragile freshwater aquifers.
In these distinct environments, primary cementing establishes the permanent barrier that anchors casing strings against structural fatigue, isolates productive gas zones, prevents inter-zonal methane migration, and protects casing tubulars from corrosive formation fluids containing carbon dioxide (CO₂) and saline brines. If a cement slurry dehydrates prematurely downhole or fails to transition rapidly from liquid to solid, annular gas channeling can compromise wellhead seals, generate sustained casing pressure (SCP), and risk environmental contamination.
Consequently, securing an experienced Australia cementing service is a vital requirement for upstream operating companies. Achieving lifelong zonal isolation demands tailored chemical formulations, high-reliability field pumping equipment, and rigorous laboratory simulation testing. By validating slurry performance using specialized chemical additives and certified HPHT consistometers, operators ensure that cement slurries maintain stable pumpability, displace drilling mud completely, and cure into durable, impermeable stone sheaths.
1. Worley Limited: Global Engineering Integration and Project Management
Worley Limited is an Australian-headquartered global engineering, procurement, and project management enterprise delivering complex energy solutions from conceptual well design to field decommissioning. While renowned for managing mega-scale LNG infrastructure and offshore platforms, Worley's well engineering specialists provide critical oversight for well construction integrity and cementing program architecture.
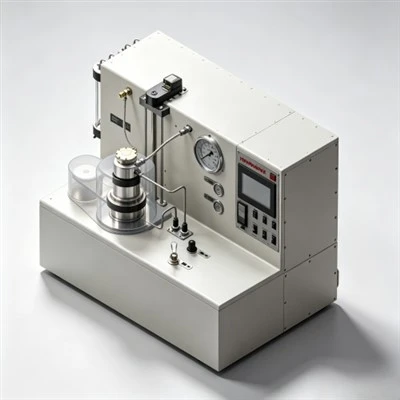
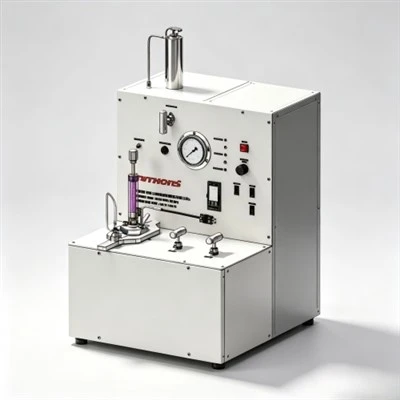
In deepwater and complex onshore field developments, Worley's engineering programs emphasize slurry systems that ensure precise fluid loss control, predictable setting kinetics, and long-term chemical durability against acid gas attack. Pumping operations rely on multi-component chemical additive packages-such as AMPS-based synthetic fluid loss additives, high-temperature retarders, multi-functional dispersants, weighted spacers, and anti-gas migration latex. Rigorous laboratory simulation on high-temperature, high-pressure consistometers ensures that slurry behavior is thoroughly qualified before mobilizing to field locations. Industry suppliers, including KELIOIL for advanced chemical additives and NITHONS for certified laboratory testing instruments, provide the technical foundation to meet these exacting standards.
2. Hilands Coal Seam Cementing: Dedicated Unconventional Gas Zonal Sealing
Hilands specializes in delivering tailored cementing and pressure pumping services for coal seam gas (CSG) and coal bed methane (CBM) projects, particularly across Queensland's Surat and Bowen basins. Shallow coal seams present delicate fracture gradients and extensive cleat permeability, requiring non-damaging slurry formulations.
When delivering an unconventional Australia cementing service, Hilands formulates lightweight (1.30 to 1.50 g/cm³) thixotropic cement systems that prevent formation invasion into fragile coal cleats while achieving an impermeable hydraulic barrier to stop shallow methane channeling. Pre-job laboratory testing with HPHT consistometers and atmospheric fluid loss cells validates that slurries maintain rapid thixotropic gel strength development after placement, isolating overlying freshwater aquifers from gas-bearing seams.
3. Wellpro Services Pty Ltd: Remedial Cementing and Well Intervention Expertise
Wellpro Services is a prominent Australian provider of coiled tubing, well intervention, and remedial cementing operations supporting both mature onshore fields and offshore platforms. Their operational focus centers on restoring well integrity, repairing casing leaks, and re-establishing zonal isolation in aging production wells.
Executing a specialized remedial Australia cementing service, Wellpro utilizes micro-fine cement formulations and low-viscosity polymeric dispersants to perform targeted squeeze operations through narrow perforations and casing splits. Pumping operations require exact control over thickening time and fluid loss to prevent slurry dehydration before the cement penetrates deep into channels behind casing. Laboratory evaluation ensures that slurry designs deliver high early compressive strength to minimize waiting-on-cement (WOC) downtime.
4. Auscoil: Integrated Drilling Support and Well Construction Services
Auscoil provides comprehensive well construction, coiled tubing drilling support, and pressure pumping services across central and western Australian operating areas, including the Cooper-Eromanga Basin.
In active onshore drilling programs, Auscoil coordinates primary casing cementing operations where borehole stability and rapid strength development are critical. Pumping operations demand stable slurry rheology, efficient mud displacement, and low API fluid loss (<40 mL/30 min) to protect water-sensitive sandstone formations. Laboratory testing on calibrated consistometers confirms that the slurry remains fully pumpable across dynamic displacement times, safeguarding casing strings from annular voids.
5. Oilfield Technologies Pty Ltd: Well Integrity Consulting and Slurry Verification
Oilfield Technologies Pty Ltd is an Australian technical consultancy and laboratory testing specialist focusing on well integrity diagnostics, completions engineering, and cementing quality assurance.
When operators evaluate an Australia cementing service, Oilfield Technologies provides independent third-party laboratory verification of cement slurry systems. Using certified HPHT consistometers, Ultrasonic Cement Analyzers (UCA), and rotational viscometers, their specialists analyze thickening time repeatability, free water breakout, and compressive strength progression under downhole temperature and pressure schedules, mitigating risk before field mobilization.
6. Condor Energy: Regional Field Engineering and Fluid Management
Condor Energy delivers integrated oilfield services, specialized drilling fluids, and cementing project support across Australia's onshore and offshore sectors, with strong operational experience in Western Australia and the Northern Territory.
Providing a dependable Australia cementing service, Condor Energy focuses on chemical spacer design, mud-to-cement displacement optimization, and gas-tight slurry formulations. By utilizing multi-functional surfactant flushes and high-performance retarders, their field operations ensure 100% circumferential mud displacement in horizontal wellbores, eliminating channel formation and protecting long-term well productivity.
Technical Matrix: Downhole Operating Parameters Across Major Australian Basins
The table below provides a systematic overview of primary downhole challenges, operating parameters, and required cement slurry technologies across Australia's major hydrocarbon basins:
Regional Application Case: Deepwater HPHT Production Liner Cementing in the Browse Basin, Offshore Australia
Case Application: Deepwater HPHT Gas Play, Browse Basin, Western Australia

Target Formation: Deep HPHT Gas Sandstones (5,100 m Depth, 160°C BHST, Narrow ECD Window)
Regional Cementing Background in Australian Offshore Deepwater Plays
In the Browse Basin located on Australia's North West Shelf, exploration and development wells penetrate overpressured gas-bearing carbonate and sandstone formations at depths exceeding 5,100 meters (16,700 feet). Water depths exceed 500 meters. Downhole conditions are severe: bottom-hole static temperatures (BHST) reach 160°C (320°F) with reservoir pressures exceeding 11,800 psi (81.4 MPa). The formations produce high-pressure gas containing CO₂ (up to 12%). The operational window between pore pressure and fracture breakdown gradient is less than 0.8 ppg. Cementing 7-inch production liners across the reservoir requires heavy Class G slurry systems (2.05 to 2.12 g/cm³) stabilized by advanced synthetic polymers.
Regional Cementing Challenges in Extreme HPHT Formations
An Australia cementing service executing production liner jobs across these deep Browse Basin reservoirs encounters critical operational hurdles:
- Severe Retarder Sensitivity: At temperatures above 150°C, minor variations of 0.05% BWOC in chemical retarder concentration cause large swings in thickening time, risking premature flash setting or multi-day setting delays.
- Narrow Equivalent Circulating Density (ECD) Windows: Close margins between formation pore pressure and fracture breakdown pressure demand low-viscosity slurries that maintain steady rheology without premature gelation spikes.
- Risk of High-Pressure Gas Channeling: An extended transition time during slurry phase changes allows gas invasion into the decaying hydrostatic column, creating sustained casing pressure (SCP).
Technical Requirements for Slurry Qualification
To qualify a heavy 2.08 g/cm³ (17.3 ppg) Class G cement system across the gas zone, the operator established strict performance criteria:
- Thickening time validation on an HPHT consistometer confirming a pumpability window of 5 hours and 30 minutes to 70 Bc under simulated dynamic ramp schedules.
- API fluid loss control strictly below 35 mL/30 min at 160°C using an automated high-temperature stirred fluid loss cell to prevent dehydration.
- Static gel strength (SGS) transition window (from 100 to 500 lbf/100 ft²) of less than 30 minutes, with 24-hour compressive strength exceeding 3,500 psi (24.1 MPa).
How Strategic Chemical Engineering Resolved the Field Challenge
To resolve these operational challenges, the central engineering laboratory executed a comprehensive qualification program using NITHONS HPHT consistometers and KELIOIL specialized cementing chemicals. Initial formulations using conventional modified lignosulfonates suffered thermal degradation, showing an erratic thickening curve that spiked past 50 Bc within 2 hours.
The team redesigned the slurry using KELIOIL synthetic AMPS-based high-temperature retarders (0.85% BWOC) paired with KELIOIL salt-resistant fluid loss additives (1.8% BWOC), sulfonated dispersants, and anti-gas migration latex. Testing on the HPHT consistometer confirmed an ideal right-angle set profile, maintaining baseline consistency at 18 Bc for 4 hours and 30 minutes before rising sharply to 70 Bc at 5 hours and 38 minutes. Ultrasonic testing on a UCA verified that the slurry reached 500 psi compressive strength in 9 hours and surpassed 3,850 psi at 24 hours.
During field execution, the Australia cementing service pumped and displaced the slurry across the 1,020-meter liner without surface pressure surges or ECD spikes. Post-job radial acoustic cement bond logs (CBL-VDL) confirmed 100% circumferential bonding across the high-pressure gas reservoir. Subsequent pressure testing recorded zero sustained casing pressure, demonstrating that rigorous laboratory qualification and advanced chemical design eliminate cementing failures in deep offshore reservoirs.
Laboratory Standards and Pre-Job Quality Assurance
Achieving reliable field execution across Australia's onshore and offshore projects requires adhering to standardized API RP 10B-2 laboratory workflows prior to job mobilization:
- Pressurized Consistometer Profiling: Slurries must be tested on calibrated HPHT consistometers using actual rig mix water and delivered cement batches to ensure thickening time repeatability.
- High-Temperature Stirred Fluid Loss: Filtration is measured under 1,000 psi differential nitrogen pressure across a 325-mesh screen to verify that API fluid loss remains strictly below 35 mL/30 min.
- Static Gel Strength Analysis: Measuring gel strength buildup confirms that the transition time between 100 and 500 lbf/100 ft² is minimized, preventing gas percolation.
- Acoustic Compressive Strength Testing: Slurry samples cured in an Ultrasonic Cement Analyzer (UCA) under static temperature must achieve 500 psi strength within 12 to 16 hours to prevent excessive waiting-on-cement time.
Frequently Asked Questions (FAQ) Regarding Australian Cementing Operations
1. Why is coal seam gas (CSG) cementing in Queensland technically challenging?
Coal seams are naturally fractured, friable, and underpressured. Standard-density cement slurries induce severe hydraulic fracturing, causing massive lost circulation and formation damage. An Australia cementing service operating in CSG fields must deploy ultra-lightweight (1.30 to 1.45 g/cm³), thixotropic slurries formulated with hollow ceramic microspheres that seal coal cleats without fracturing the pay zone.
2. How does CO₂ presence in Browse Basin gas impact cement sheath design?
High concentrations of subterranean carbon dioxide (CO₂) dissolve in formation brines to form carbonic acid (H₂CO₃), which leaches calcium hydroxide from cured Portland cement, causing carbonation and matrix degradation. Formulating cement systems with silica flour, pozzolanic materials, and synthetic latex additives forms an impermeable, low-calcium-ratio sheath that resists acid gas leaching.
3. What is the role of HPHT consistometer testing in Australian offshore projects?
An HPHT consistometer simulates dynamic bottom-hole circulating temperature (BHCT) and hydrostatic pressure ramps, verifying that the cement slurry remains pumpable (<30 Bc) throughout multi-hour displacement while confirming an engineered 90 to 120-minute safety cushion before reaching the 70 Bc pumpability limit.
Strategic Collaboration for Safe Well Construction
As well construction across Australia expands into deeper offshore reservoirs, complex gas plays, and high-temperature formations, achieving multidecade well integrity depends directly on selecting a qualified Australia cementing service supported by robust laboratory testing and specialized chemistry.
Through the combination of KELIOIL high-performance cementing additives and NITHONS laboratory testing instruments, operators and service companies across Australia gain access to reliable chemical solutions and certified testing systems that ensure successful slurry placement, protect subterranean environments, and maximize long-term asset productivity.
Equip Your Operations with KELIOIL Additives & NITHONS Laboratory Systems
Our technical specialists provide customized slurry formulation designs, API Spec 10A laboratory testing equipment, and bulk chemical supply of premium cementing additives tailored to demanding onshore and offshore drilling operations across Australia.